
Optimize quality, minimize costs.
Engineering solutions for the manufacture and repair of molds and dies.
Higher productivity and better finishes with fewer passes and operations, resulting in lower tool and cutting fluid consumption
Greater lubricity allows for
- Extend the service life of tools.
- Use more aggressive cutting parameters and reduce cycle time.
- Reduce the number of passes required to achieve the desired roughing/finishing.
- Improve surface finish and reduce workpiece roughness.
- Potential to streamline processes.
Greater emulsion stability
- Prevents the formation of unpleasant odors without the use of chemicals such as bactericides.
- Prevents the formation of residue and protects against corrosion.
- Reduces monthly concentrate consumption by up to 35%.
- Significantly lowers total spending on cutting fluids
Proven solutions for mold and die machining
B-Cool MC 600
- Designed for manufacturing operations involving molds and dies.
- Ideal for all types of steel and aluminum.
- Service life of at least 12 months.
- Working concentration of 8–10%.
- Typical dilution ratio: 2.5% (2.5 liters per 100 liters of water).
B-Cool MC 610
- Recommended for high-alloy steels, titanium, and molds with high finish requirements.
- All types of steel, stainless steel, and aluminum.
- Shelf life of at least 12 months.
- Working concentration of 8–10%.
- Typical dilution ratio of 2 liters per 100 liters of water (2%).
We also carry oils for electrical discharge machining (EDM).
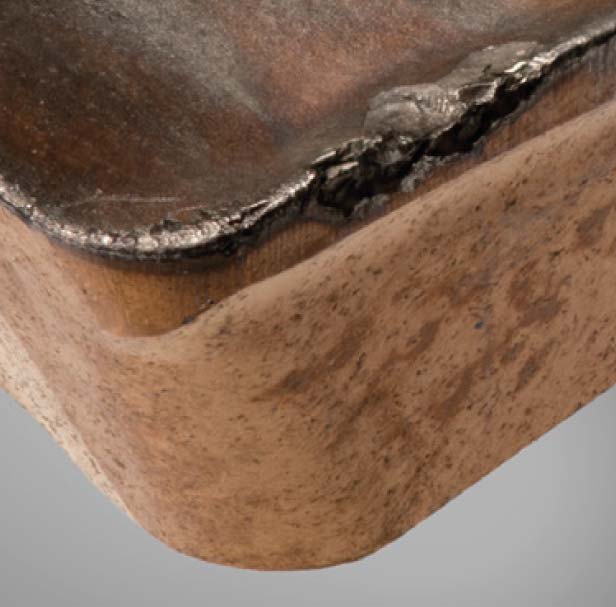
Conventional cutting fluid
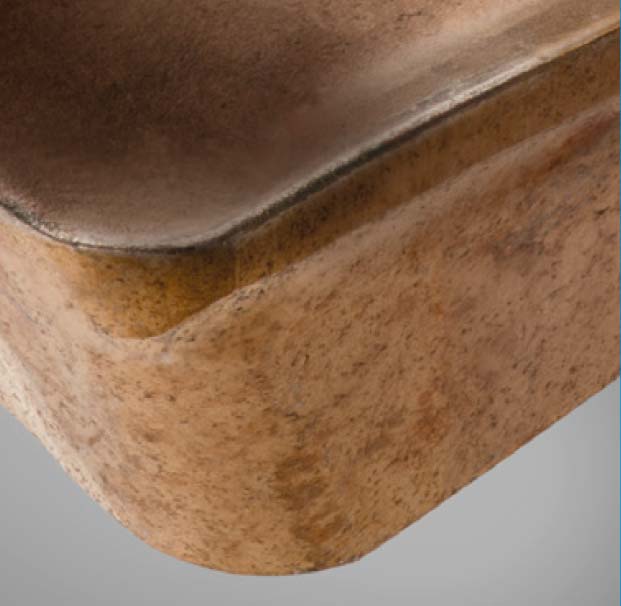
Blaser high-performance cutting fluid
Longer tool life
- Less premature tool wear.
- Lower tooling cost per part.
- Increased machine production capacity.